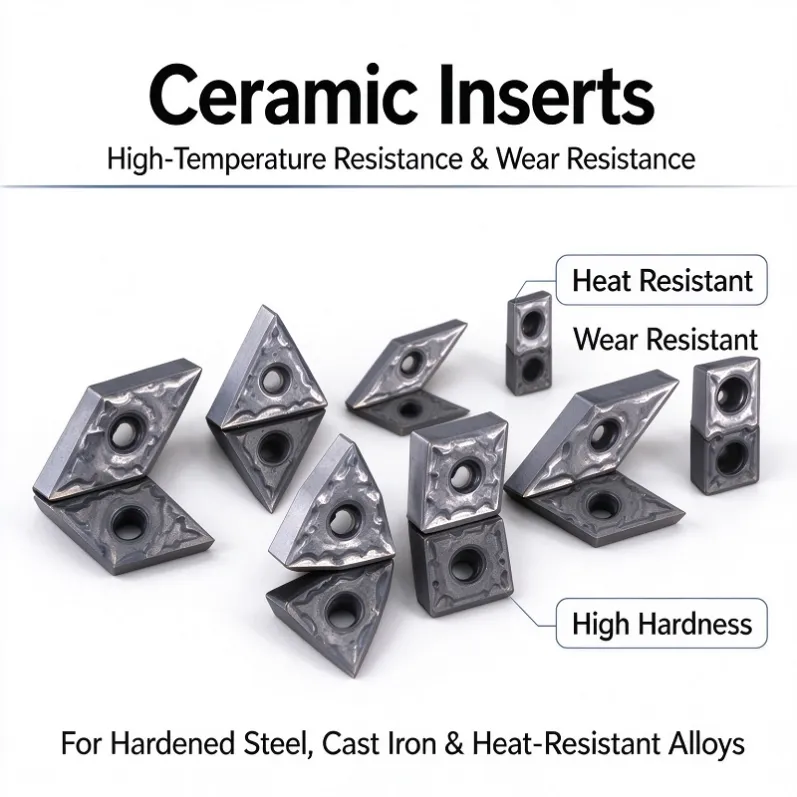
Ceramic Inserts
High-Temperature Resistance & Wear Resistance Ceramic Turning Inserts
Product Features 1. Improved hot hardness and shock resistance, maintaining excellent stability even under harsh cutting conditions. 2. Substrate reinforcement technology greatly enhances bonding strength, delivering outstanding chipping and wear resistance to achieve high-quality finished surface.
Specifications
- Machinable Hardness:
- HRC 23~34
- Workpiece Materials:
- Alloy steel, Cast iron
- Machining Type:
- Turning
- Equipment:
- CNC Lathe
Product Overview
These ceramic inserts are manufactured with high-tech nanotechnology and precision ceramic high-pressure sintering process. Featuring high hardness (Mohs hardness 9), high density, high temperature resistance, anti-magnetization and anti-oxidation properties. Suitable for semi-finishing & finishing with low impact and continuous cutting.
Product Classification
| Application | Grade | | Characteristics | |
|---|---|---|---|---|---|
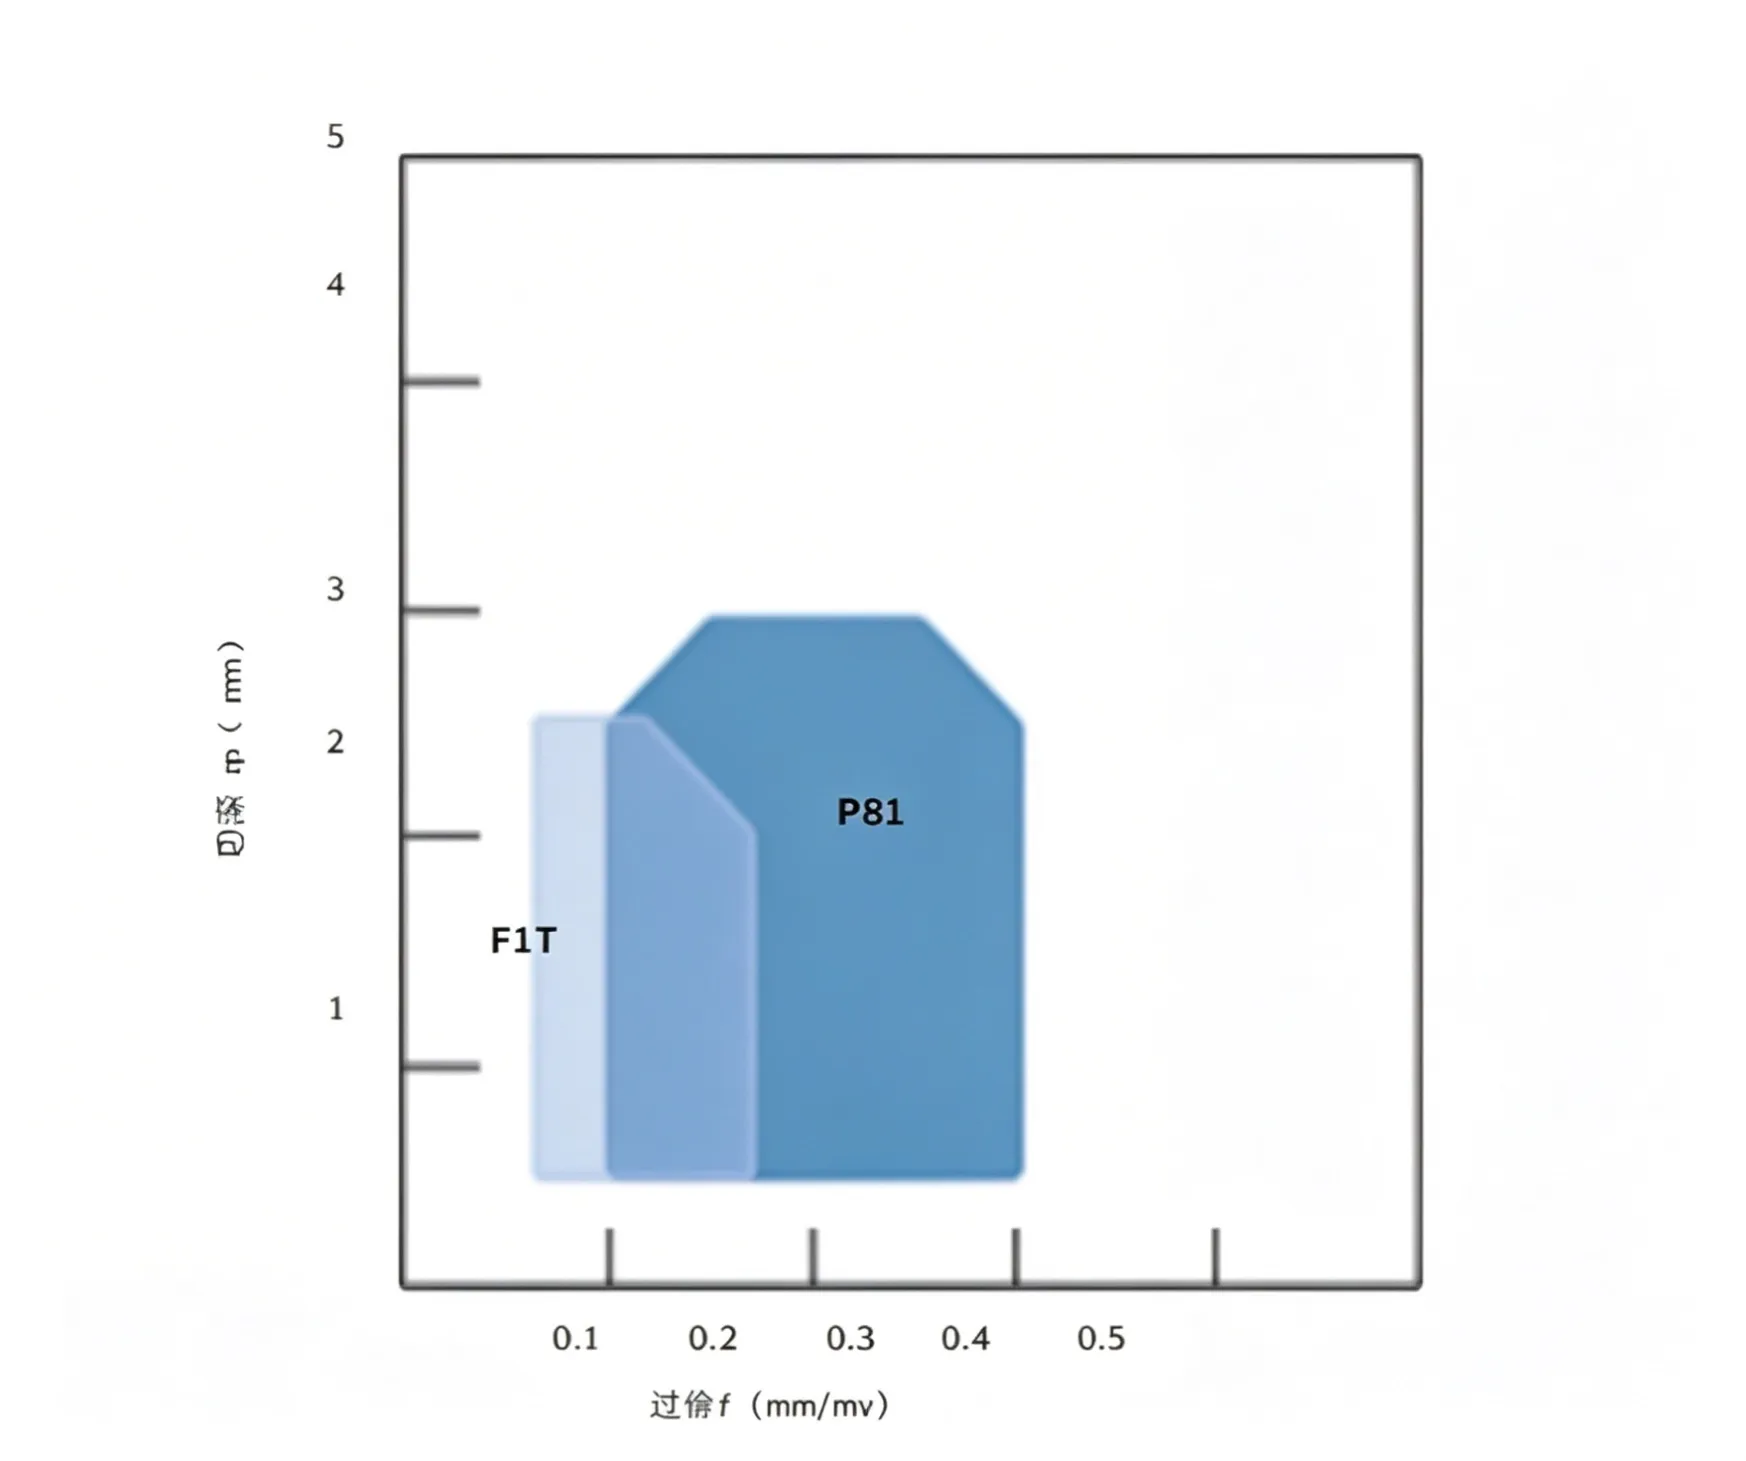 | Finishing | F1T |  | For finishing, good chip control under small depth of cut | 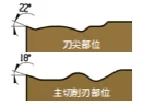 |
Finishing | PB1 |  | General-purpose chipbreaker for finishing with high stability | 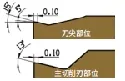 | |
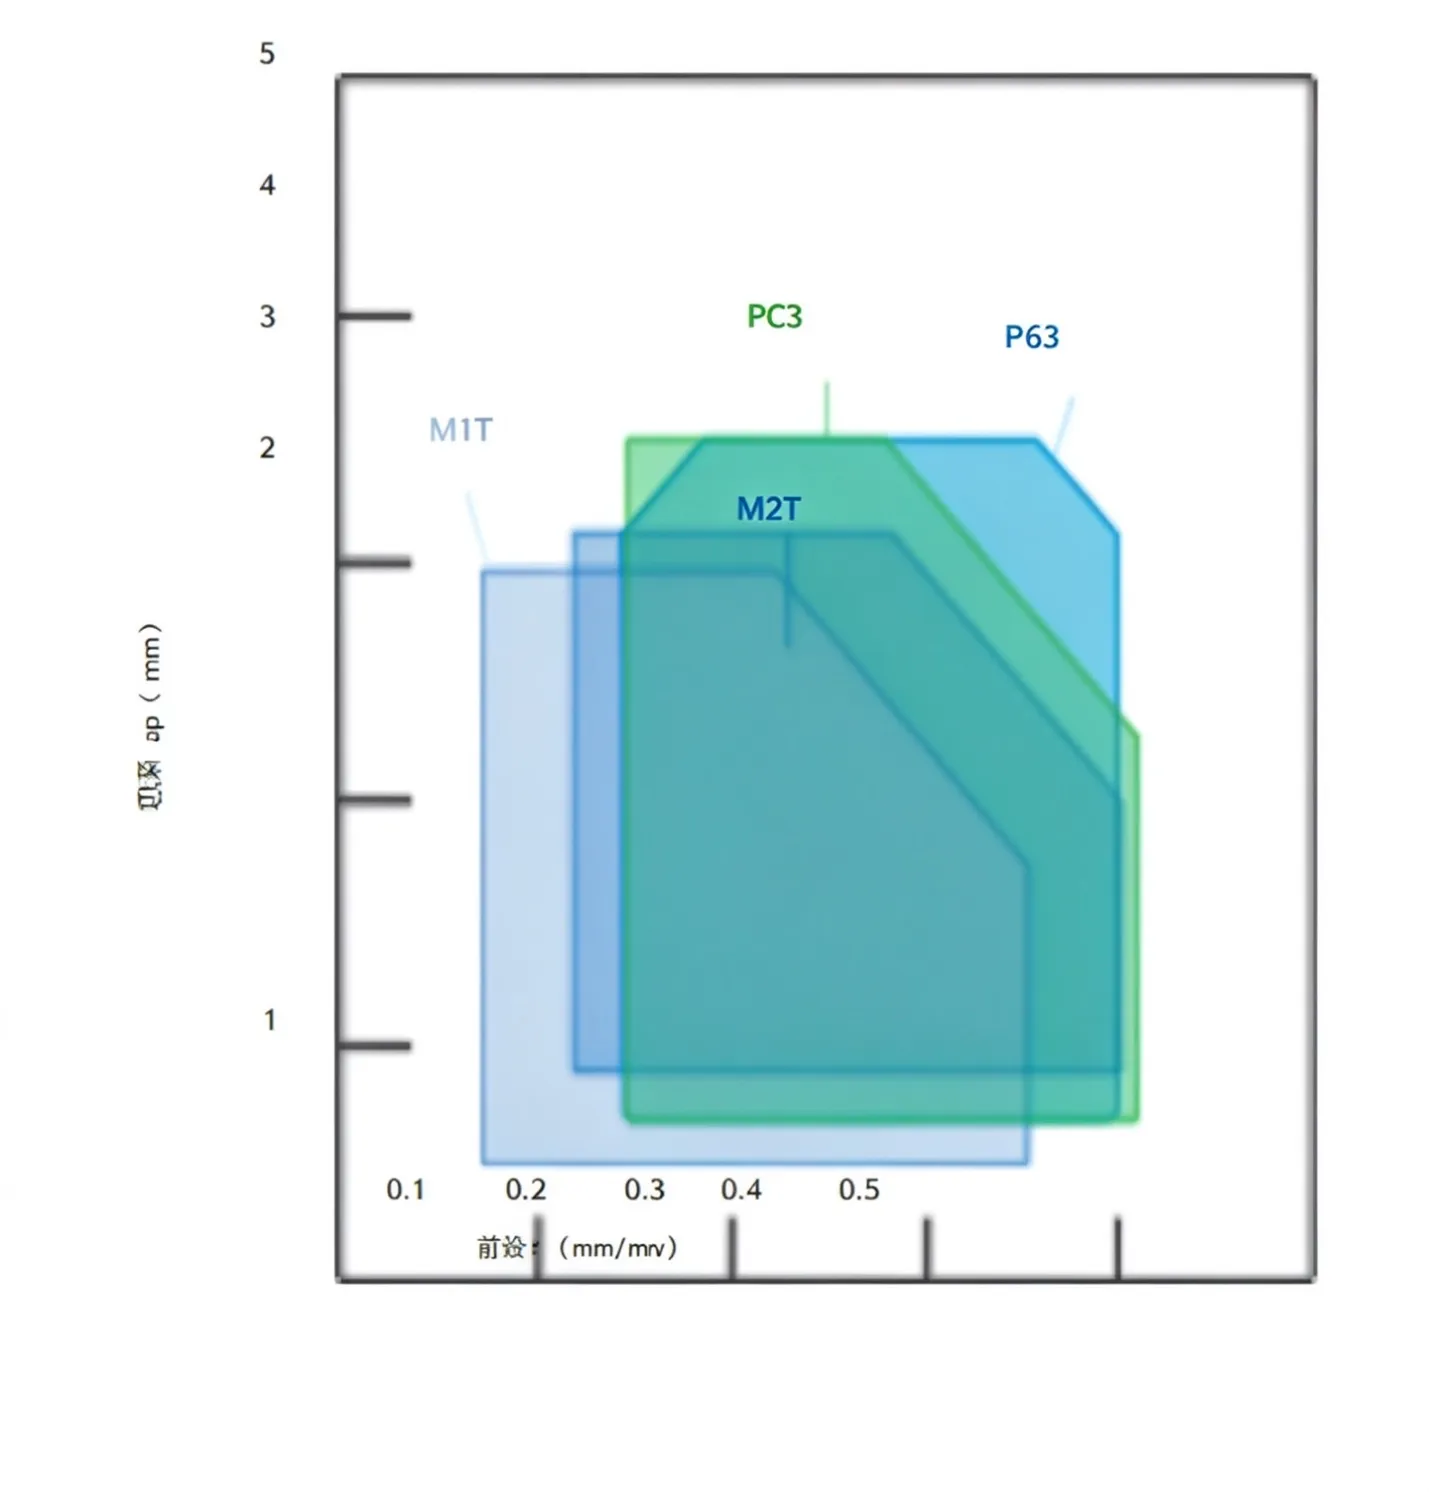
Semi-finishing | M1T |  | Large rake angle & low cutting force, adaptable for variable cutting depth |  | |
 | Semi-finishing | PB3 |  | 1st recommended chipbreaker for semi-finishing of steel; good chip handling for profiling & variable depth cutting |  |
Semi-finishing | M2T |  | Low cutting resistance with strong cutting edge, for medium machining with large depth of cut |  | |
Semi-finishing | PC3 |  | 2nd recommended chipbreaker for semi-finishing of steel |  | |
Medium Machining | PD3 |  | High edge strength with reliable stability, available for interrupted cutting |  | |
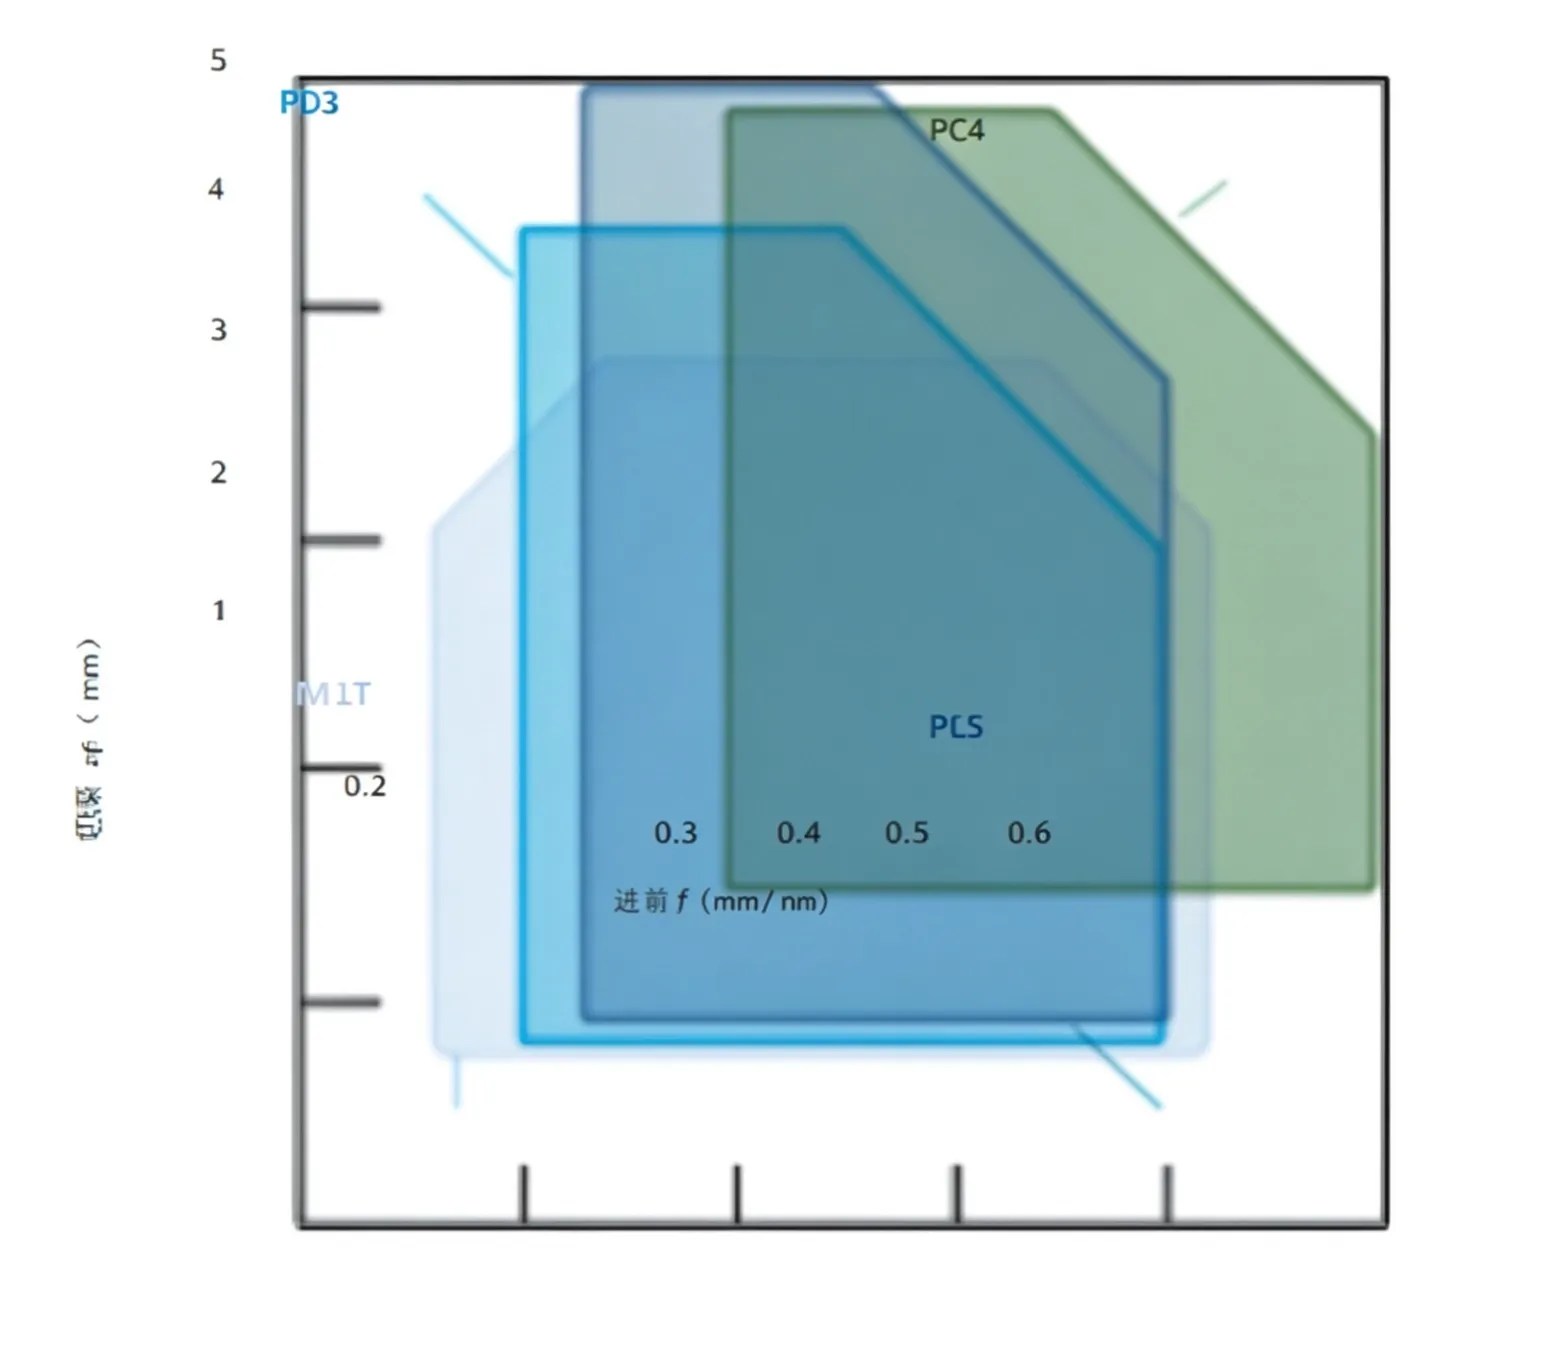 | Medium Machining | M3T |  | Smooth rake angle, suitable for high feed medium machining | 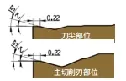 |
Medium Machining | PC4 | 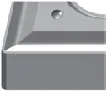 | Full peripheral chipbreaker, low cutting resistance, universal for steel & cast iron | 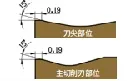 | |
Medium Machining | PL5 | 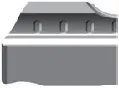 | Low resistance & large depth of cut, ideal for long shaft workpieces | 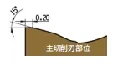 |
Product Specifications
Blade | Insert Model | d(mm) | s(mm) | d1(mm) | r(mm) |
|---|---|---|---|---|---|
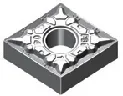 | CNMG 120404E-PB1 | 12.7 | 4.76 | 5.16 | 0.4 |
CNMG 120408E-PB1 | 12.7 | 4.76 | 5.16 | 0.8 | |
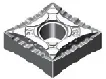 | CNMG 120404E-PB3 | 12.7 | 4.76 | 5.16 | 0.4 |
CNMG 120408E-PB3 | 12.7 | 4.76 | 5.16 | 0.8 | |
CNMG 120412E-PB3 | 12.7 | 4.76 | 5.16 | 1.2 | |
 | DNMG 110404E-PB1 | 9.525 | 4.76 | 3.81 | 0.4 |
DNMG 150404E-PB1 | 12.7 | 4.76 | 5.16 | 0.4 | |
DNMG 150408E-PB1 | 12.7 | 4.76 | 5.16 | 0.8 | |
 | DNMG 110404E-PD3 | 9.525 | 4.76 | 3.81 | 0.4 |
DNMG 110408E-PD3 | 9.525 | 4.76 | 3.81 | 0.8 | |
DNMG 150404E-PD3 | 12.7 | 4.76 | 5.16 | 0.4 | |
DNMG 150408E-PD3 | 12.7 | 4.76 | 5.16 | 0.8 | |
 | SNMG 120404E-PB1 | 12.7 | 4.76 | 5.16 | 0.4 |
SNMG 120408E-PB1 | 12.7 | 4.76 | 5.16 | 0.8 | |
 | TNMG 160404E-PB1 | 9.525 | 4.76 | 3.81 | 0.4 |
TNMG 160408E-PB1 | 9.525 | 4.76 | 3.81 | 0.8 | |
TNMG 160412E-PB1 | 9.525 | 4.76 | 3.81 | 1.2 | |
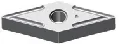 | VNMG 160404E-PC4 | 9.525 | 4.76 | 3.81 | 0.4 |
VNMG 160408E-PC4 | 9.525 | 4.76 | 3.81 | 0.8 | |
VNMG 160412E-PC4 | 9.525 | 4.76 | 3.81 | 1.2 | |
 | WNMG 080404E-PD3 | 12.7 | 4.76 | 5.16 | 0.4 |
WNMG 080408E-PD3 | 12.7 | 4.76 | 5.16 | 0.8 | |
WNMG 080412E-PD3 | 12.7 | 4.76 | 5.16 | 1.2 |
Cutting Parameters
Workpiece Material | Hardness | Cutting Speed Vc (m/min) | Material Examples |
|---|---|---|---|
Mild Steel | HB ≤180 | 150-300 | Q235, 10# steel |
Carbon Steel & Alloy Steel | HB ≥180 | 120-260 | 45#, 40CrMo |
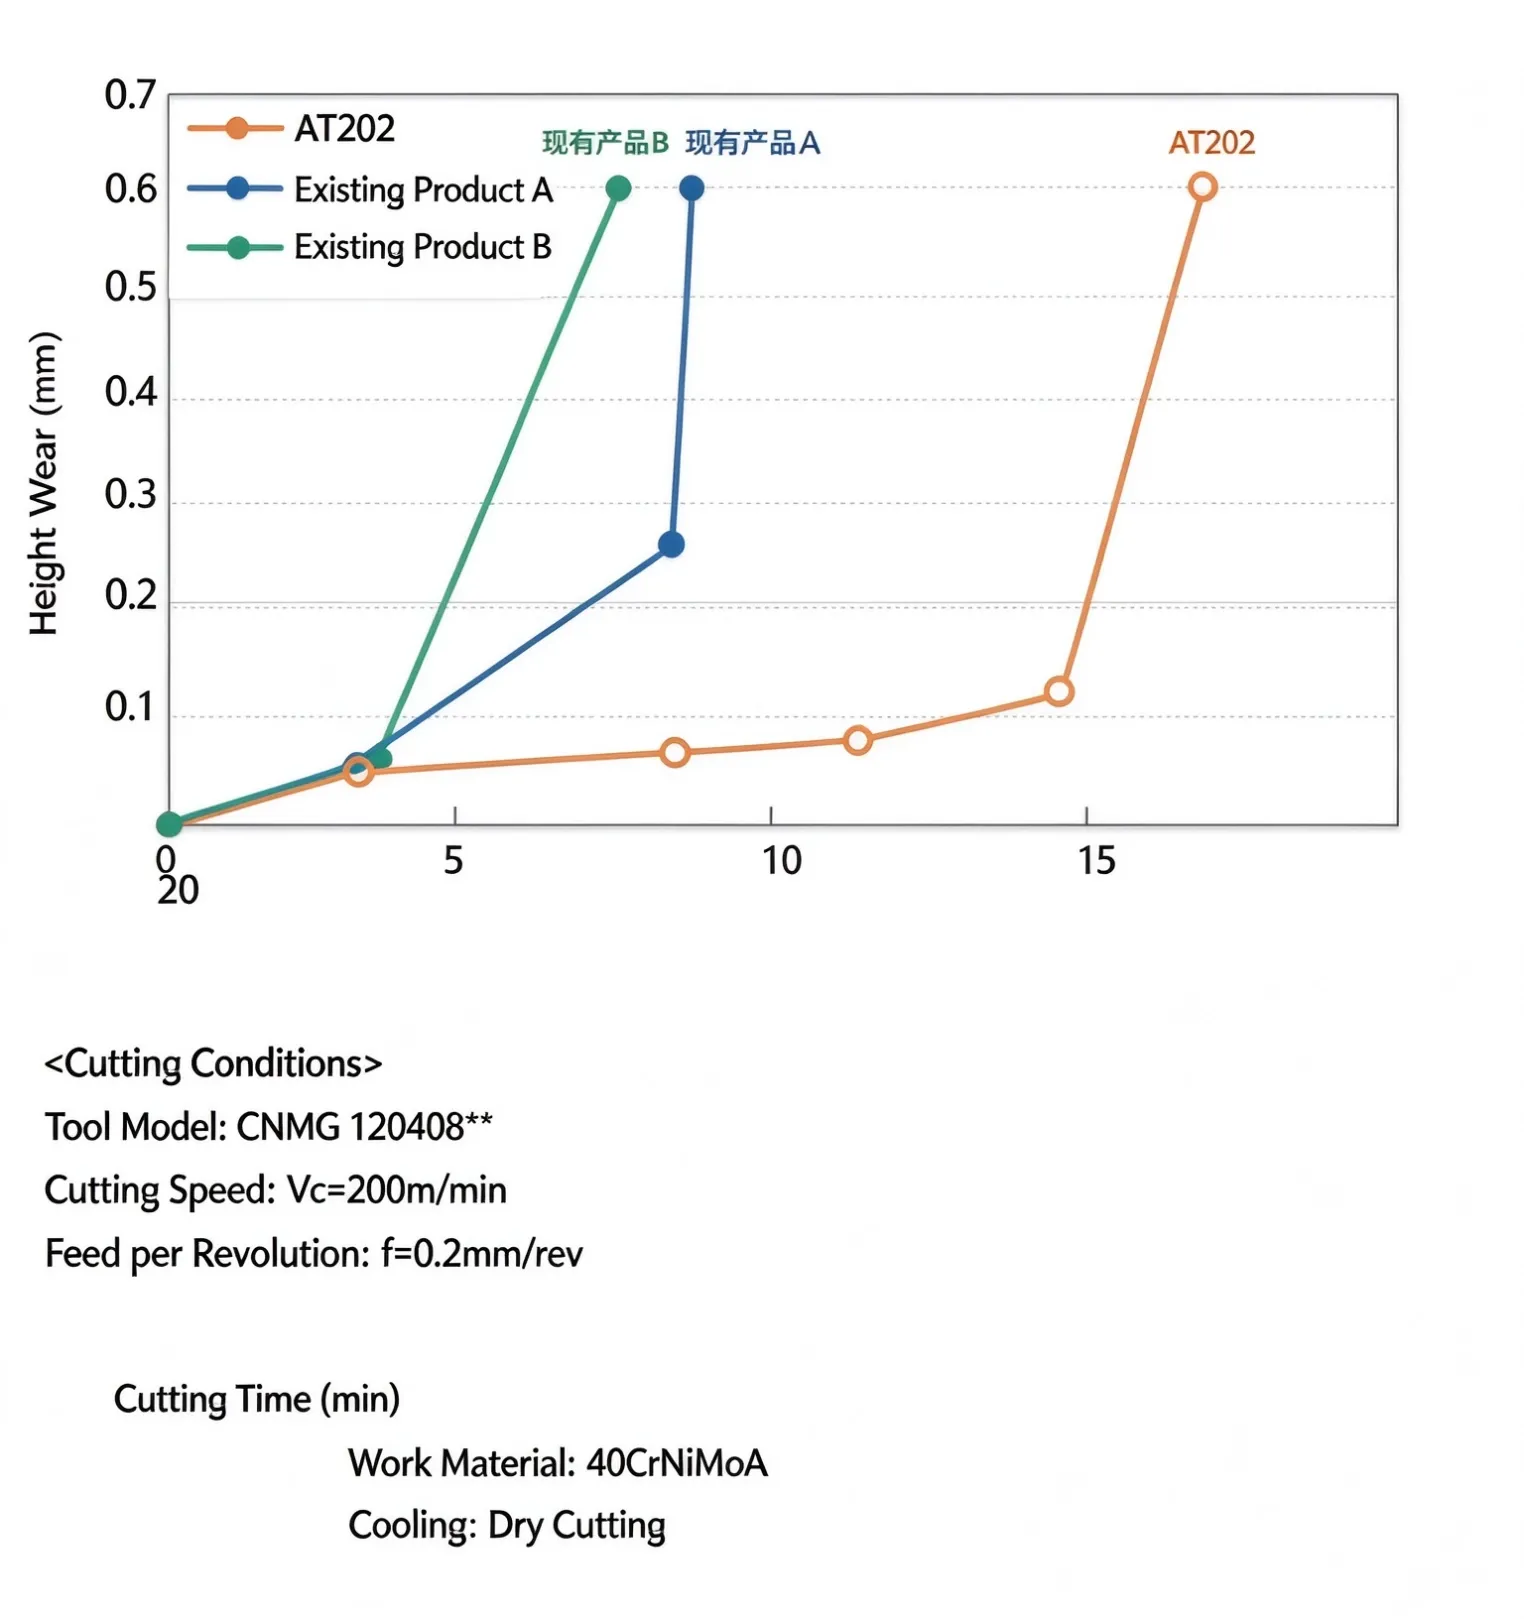
Machining Case
Comparison of Cutting Time: 18.4 minsCutting Conditions:
- Insert Model: CNMG 120408
- Cutting Speed Vc=200 m/min
- Feed per revolution f=0.2 mm/rev
- Depth of cut ap=1.0 mm
- Workpiece: 40CrNiMoA
- Cooling: Dry Cutting