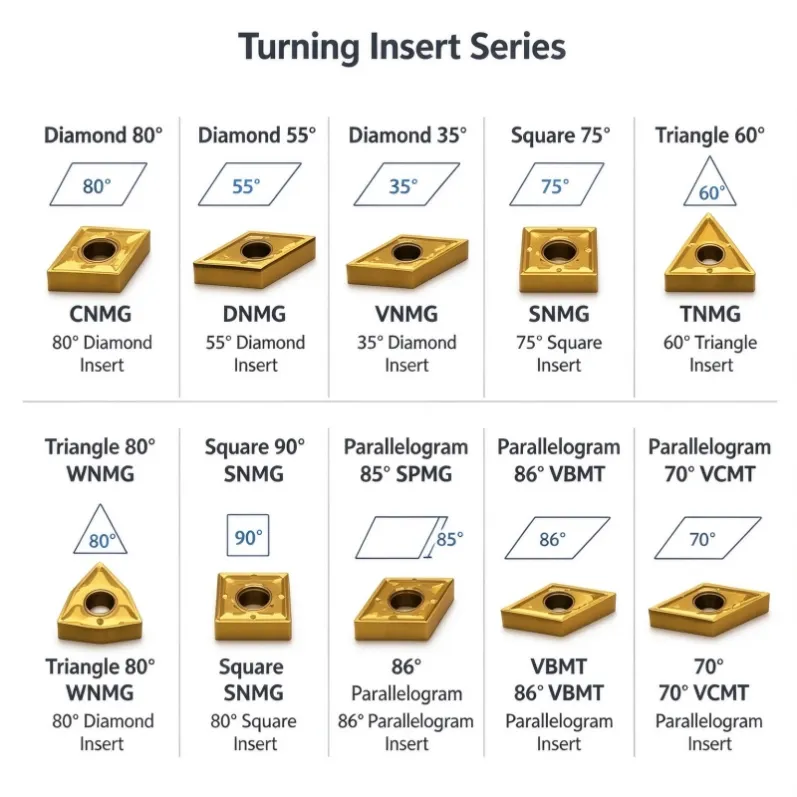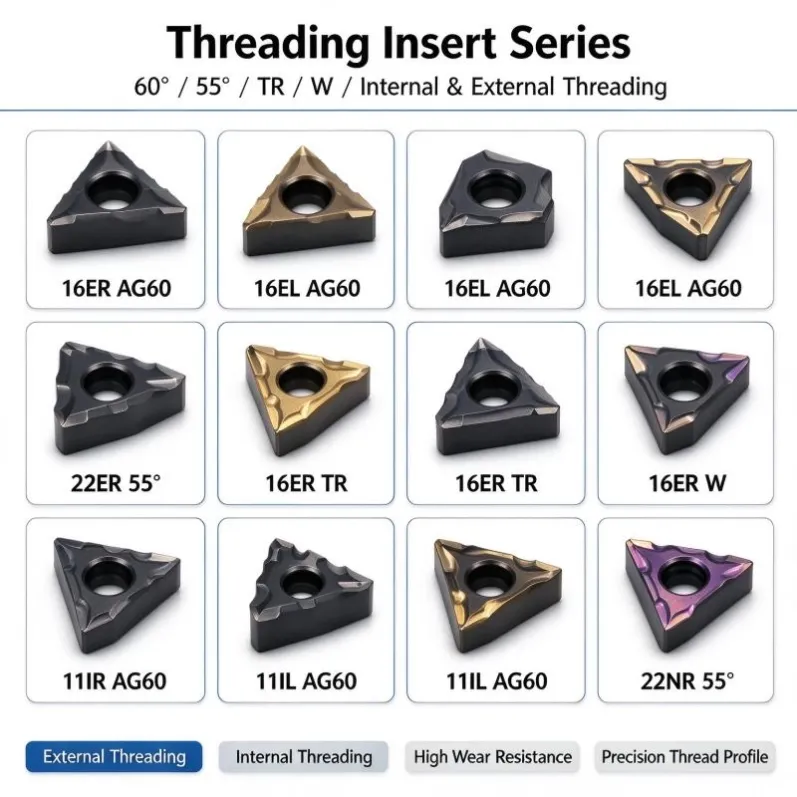
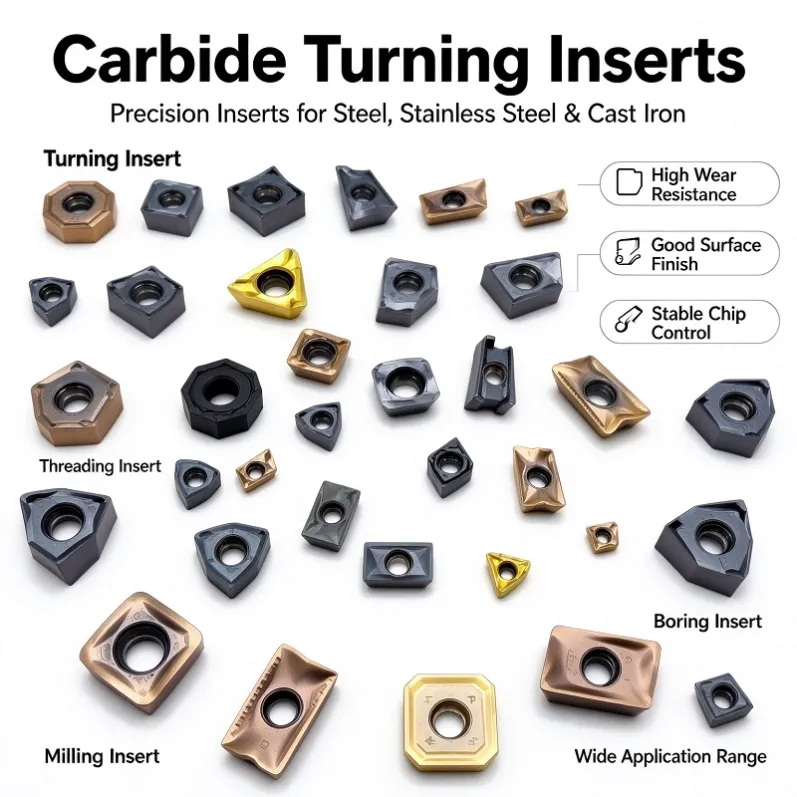
Turning / Threading / Milling Inserts
Milling Blade Inserts for Steel, Stainless Steel & Cast Iron
Through rotary movement of the cutting tool and reciprocating motion of the workpiece, surfaces or profiles meeting dimensional requirements are machined.
Specifications
- Machining Hardness:
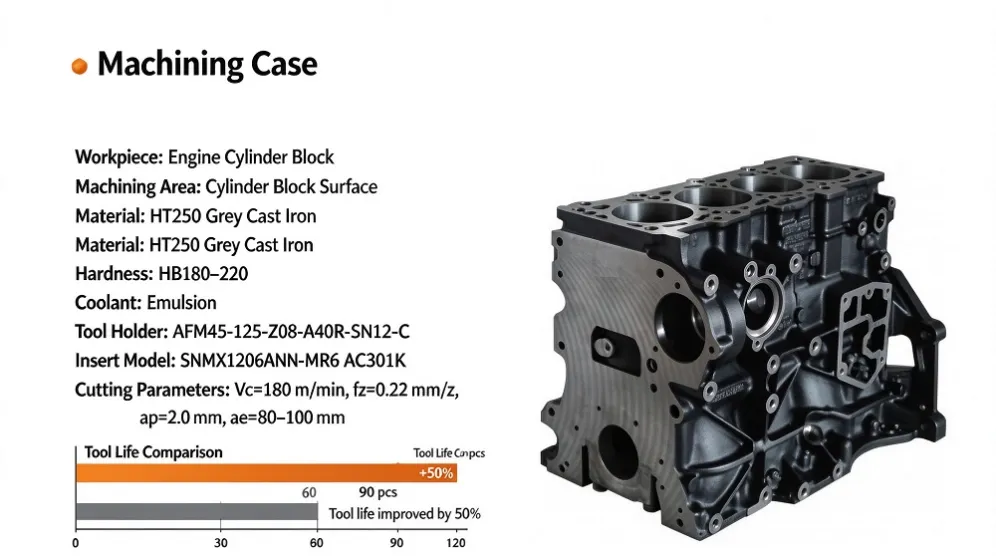
- HB180
- Work Materials:
- Ductile Iron QT550, Grey Cast Iron HT250, 316L Stainless Steel, etc.
- Machining Range:
- Face milling, profile milling
- Equipment:
- Machining Center
Milling Inserts
Application
Milling inserts act as precision cutting teeth for machine tools to machine various metals. These indexable inserts cut, slot and profile workpieces via high-speed rotating milling cutter bodies. Modern inserts adopt cemented carbide substrates with multi-layer nano coatings, delivering sharp cutting performance and long wear resistance simultaneously.
Product Parameters
Blade | Insert Model | Dimensions(mm) L(MM) / d(MM) / S(MM) / r(mm) / h(mm) | Geometry |
|---|---|---|---|
 | ROHT 0803M0E-MM3 | L:08, S:3.18 | Round |
ROHT 10T3M8E-MM3 | L:10, S:3.97 | Round | |
ROHT 1204M4E-MM3 | L:12, S:4.76 | Round | |
ROHT 1204M6E-MM3 | L:12, S:4.76 | Round | |
ROHT 1605M8E-MM3 | L:16, S:5.56 | Round | |
ROHT 2006M8E-MM3 | L:20, S:6.35 | Round | |
 | ROMT 10T3M4E-MR6 | L:10, S:3.97 | Round |
ROMT 1204M6E-MR6 | L:12, S:4.76 | Round | |
ROMT 1605M6E-MR6 | L:16, S:5.56 | Round | |
ROMT 2006M8E-MR6 | L:20, S:6.35 | Round | |
 | RPMT 1204MOE-T1000 | L:12, d:14.6 | Round |
 | LNHU 090408ER-MR2 | L:9, d:4.5, S:7.5, r:0.4 | Rhombus |
LNHU 090404ER-MM3 | L:9, d:4.5, S:7.45, r:0.8 | Rhombus | |
LNHU 090412ER-MR2 | L:9, d:4.5, S:7.4, r:1.2 | Rhombus | |
LNHU 090416ER-MR2 | L:9, d:4.5, S:7.35, r:1.6 | Rhombus | |
LNHU 090420ER-MR2 | L:9, d:4.5, S:7.31, r:2.0 | Rhombus | |
LNHU 130608ER-MR2 | L:13.02, d:6.8, S:10.15, r:0.8 | Rhombus | |
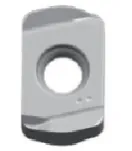 | LNMX 060410R-MM3 | L:10, d:6.35, S:3.6, r:1.0 | Rhombus |
LNMX 060410R-MM4N | L:10, d:6.35, S:3.6, r:1.0 | Rhombus | |
 | WNGU 080608R-MR2 | L:8, d:12.5, S:7.88, r:0.8 | Trigon |
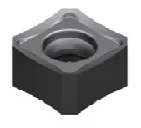 | SNMX 1206ENN-MM4 | L:12.7, S:6.34, r:1.2 | Square |
SNGX 1206ENN-MM4 | L:12.7, S:6.34, r:1.2 | Square |
Product Classification (Chip Breaker Features)
Name | Chip Breaker | Cutting Edge Geometry | Application |
|---|---|---|---|
Easy-cut Type | MM3 | 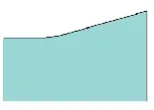 | Good working conditions & finishingLow cutting force (available for low-power machine tools)Semi-finishing / Finishing under favorable conditions, low cutting force, medium feed |
General Type | MM4 | 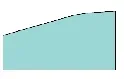 | Medium machining conditionsIdeal groove type for universal machiningSuitable for most materials under medium cutting conditions |
Heavy-duty Type | MR2 | 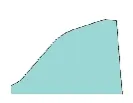 | Harsh working conditionsHigh edge stability, higher feed rate |
Stable Type | MR6 | 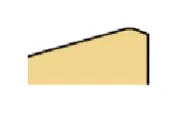 | Robust cutting edgeRoughing of steel and cast ironRecommended for unstable machining conditionsExcellent edge stability, high feed |
Sharp Type | FM2 | 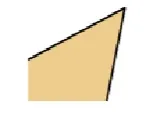 | Specially designed for aluminum machiningLow cutting force with sharp cutting edge |
Stable Type | RR2 | 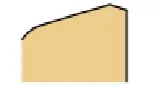 | High process reliability, suitable for castings with sand inclusions & casting skin |
Recommended Cutting Data
ISO Material Group, Grade Selection, Cutting Speed, Feed & Depth of Cut
ISO Group | Material | Tensile Strength (MPa) | Brinell Hardness (HB) | AC301K (CVD)Vc (m/min) | AP351K (PVD)Vc (m/min) | AC301U (PVD)Vc (m/min) | AC301P (CVD)Vc (m/min) | AP351U (PVD)Vc (m/min) | AP401U (PVD)Vc (m/min) | WN08Vc (m/min) | Chipbreaker Recommendation | Feed fz (mm/z)Min – Max | Depth of Cut ap (mm)Min – Max |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
P | Unalloyed Steel | <600 | <180 | 450 / 340 / 290 | 430 / 230 / 120 | 230 / 205 / 170 | — | — | — | — | MM3, MM4, MR2 | 0.12 – 0.22 | 0.6 – 8 |
P | Low Alloy Steel | <950 | <280 | 320 / 240 / 200 | 380 / 220 / 120 | 200 / 180 / 160 | — | — | — | — | MM3, MM4, MR2 | 0.12 – 0.22 | 0.6 – 8 |
P | Alloy Steel | 700 – 950 | 200 – 280 | 290 / 210 / 185 | 340 / 240 / 120 | 200 / 155 / 110 | — | — | — | — | MM3, MM4, MR2 | 0.12 – 0.18 | 0.6 – 8 |
P | Alloy Steel | 950 – 1200 | 280 – 355 | 280 / 210 / 200 | 260 / 150 / 80 | 180 / 130 / 90 | — | — | — | — | MM3, MM4, MR2 | 0.12 – 0.18 | 0.6 – 8 |
P | Alloy Steel | 1200 – 1400 | 355 – 415 | 210 / 170 / 110 | 145 / 105 / 65 | 140 / 105 / 70 | — | — | — | — | MM3, MM4, MR2 | 0.12 – 0.18 | 0.6 – 8 |
M | Duplex Stainless Steel | 778 | 230 | 165 / 150 / 130 | 225 / 180 / 125 | 270 / 215 / 155 | 150 / 115 / 85 | — | — | — | MM3, MM4, MR2 | 0.12 – 0.16 | 0.6 – 8 |
M | Austenitic Stainless Steel | 675 | 200 | 270 / 185 / 90 | 210 / 145 / 75 | 260 / 180 / 90 | 185 / 140 / 105 | — | — | — | MM3, MM4, MR2 | 0.12 – 0.12 | 0.6 – 8 |
M | Precipitation Hardening Stainless Steel | 1013 | 300 | 300 / 225 / 165 | 140 / 130 / 90 | 170 / 150 / 110 | 125 / 95 / 70 | — | — | — | MM3, MM4, MR2 | 0.12 – 0.20 | 0.6 – 8 |
K | Grey Cast Iron | 700 | 220 | 480 / 310 / 140 | 390 / 280 / 130 | 370 / 280 / 130 | 310 / 210 / 90 | 290 / 220 / 150 | — | — | MM3, MM4, MR2 | 0.12 – 0.20 | 0.6 – 8 |
K | Ductile Iron | 880 | 260 | 450 / 295 / 140 | 350 / 250 / 120 | 370 / 260 / 130 | 290 / 190 / 100 | 180 / 130 / 70 | — | — | MM3, MM4, MR2 | 0.12 – 0.18 | 0.6 – 8 |
K | Malleable Cast Iron | 800 | 250 | 336 / 220 / 100 | 270 / 200 / 100 | 410 / 320 / 210 | 310 / 240 / 150 | 390 / 300 / 190 | — | — | MM3, MM4, MR2 | 0.12 – 0.13 | 0.6 – 8 |
S | Iron-based Superalloy | 943 | 280 | 50 / 40 / 30 | 45 / 40 / 30 | — | — | — | — | — | MM3, MM4, MR2 | 0.12 – 0.12 | 0.6 – 8 |
S | Cobalt-based Superalloy | 1076 | 320 | 45 / 38 / 30 | 45 / 40 / 30 | — | — | — | — | — | MM3, MM4, MR2 | 0.12 – 0.12 | 0.6 – 8 |
S | Nickel-based Superalloy | 1177 | 350 | 45 / 38 / 30 | 45 / 40 / 30 | — | — | — | — | — | MM3, MM4, MR2 | 0.12 – 0.13 | 0.6 – 8 |
S | Titanium Alloy | 1262 | 370 | 100 / 75 / 30 | 100 / 70 / 45 | — | — | — | — | — | MM3, MM4, MR2 | 0.12 – 0.13 | 0.6 – 8 |
N | Aluminum Alloy | 447 | 130 | — | — | — | — | — | — | — | FM2 | 0.10 – 0.30 | 0.6 – 8 |
H | Hardened Steel | — | 50–60 HRC | — | — | — | — | — | — | — | MR2 | 0.08 – 0.15 | 0.2 – 1 |
H | Chilled Cast Iron | — | 55 HRC | — | — | — | — | — | — | — | MR2 | 0.08 – 0.15 | 0.2 – 1 |
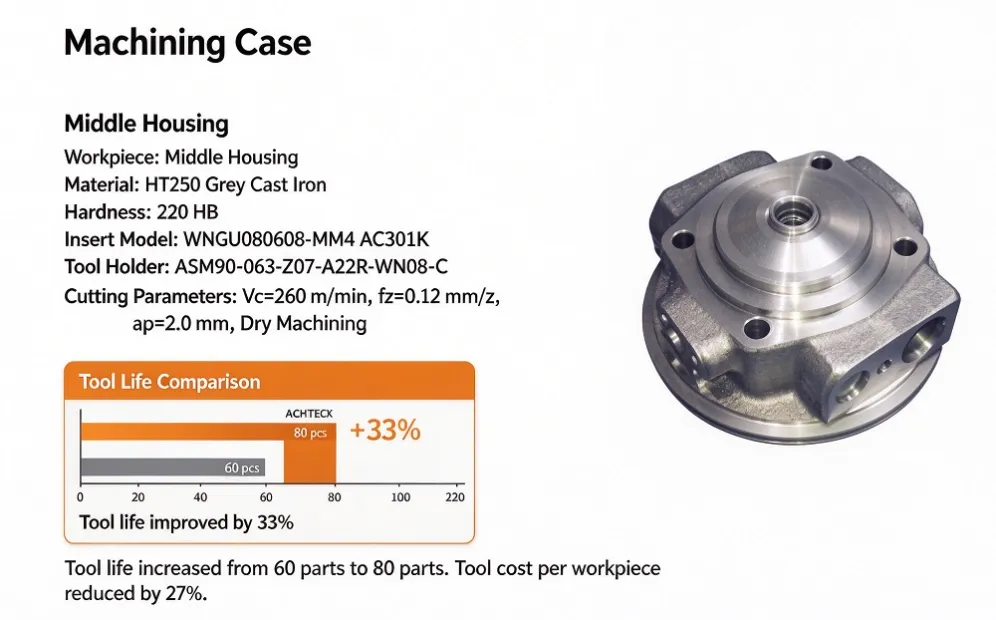
- Workpiece: Middle Housing
- Material: HT250 Grey Cast Iron
- Insert: WNGU080608-MM4 AC301K
- Result: Tool life improved by +33%