Taps
Precision Taps for Steel/Stainless Steel/Cast Iron/Aluminum
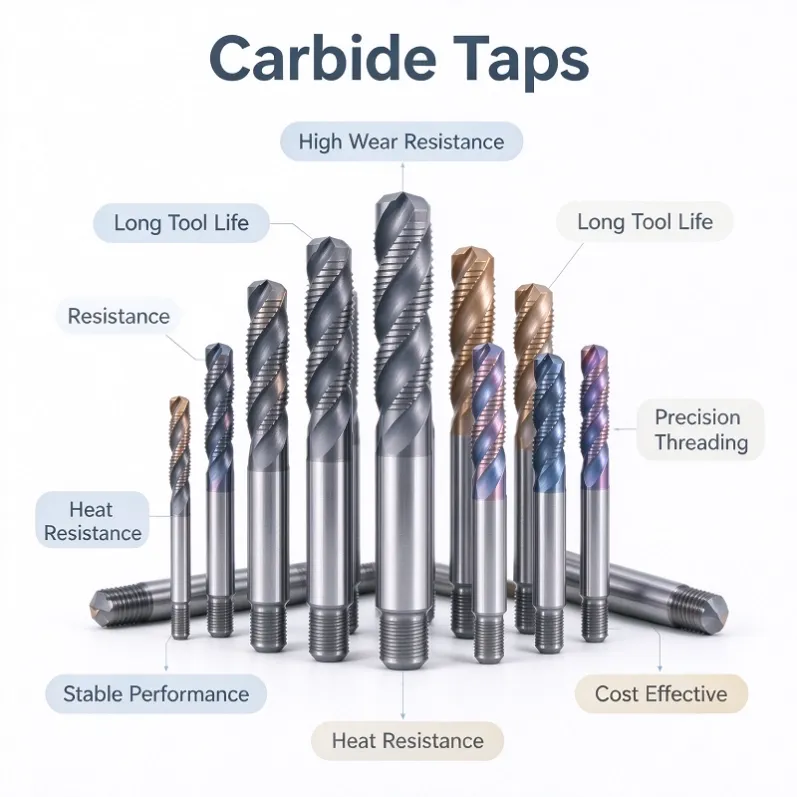
A tap is a cutting tool used to machine internal threads in pre-drilled holes. It forms the required thread profile through rotational movement and axial feed, and is widely applied in mechanical manufacturing and assembly industries.
Specifications
- Straight Flute Tap:
- Easy to machine, suitable for both through holes and blind holes. Lower cutting speed and slightly reduced precision.
- Spiral Flute Tap:
- Optimized for blind hole machining. It enables smooth chip evacuation, supports fast cutting speed and delivers high precision.
- Spiral Point Tap (Gun Tap):
- Features chip grooves at the front end. Designed for through-hole applications with low cutting torque and superior thread surface finish.
- Rake Angle Taps & Pipe Thread Taps:
- For special thread profiles or pipe component machining.
Application Purposes
Taps are mainly used to cut internal threads on workpieces, enabling secure assembly of bolts and screws.
- Fabricate nuts or threaded holes
- Repair or rework existing threads
Select the proper tap type based on workpiece material and hole depth to improve machining efficiency and thread quality.
Tap selection must consider hole type (through or blind hole), material hardness, thread specification and machining tolerance requirements. Proper use of taps can significantly boost threading efficiency and quality, while extending tool service life.
Product Classification
Name | Material | Cooling Method | Type | Application | Image |
|---|---|---|---|---|---|
Cutting Tap | High Speed Steel | External Cooling | Spiral Flute Tap & Spiral Point Tap | - Made from premium high-speed steel substrate with balanced hardness and toughness. Suitable for a wide range of working conditions, including CNC machining centers, radial drilling machines, horizontal lathes.- Applicable for standard ISO P, M, K, N materialsISO P: 95 HB ‒ 300 HB (300 N/mm² ‒ 1000 N/mm²)ISO M: <238 HB (<800 N/mm²)ISO K: GJS (GGG)ISO N: Al-alloys, AlSi with Si content <4% |  |
Forming Tap | Carbide | External / Internal Cooling | Universal for Through & Blind Holes | - Suitable for ISO material groups: P, M, K, NISO P: 200 ~1200 N/mm² (primary application)ISO N: Si content <9% (primary recommendation)ISO K: Elongation at break >8% (Ductile Iron 400, GJS-400)Industries: Automotive parts, general machinery, construction machinery, energy sectorTypical components: crankshaft, connecting rod, motor shaft, flange, wheel hub bearing |  |
Product Data
Item | Spiral Point Tap | Spiral Flute Tap |
|---|---|---|
Threading Depth | ≤3.0×DN | ≤2.5×DN |
Product Line | ECO | ECO |
Series | T102 | T103 |
Reference Standard | JIS / DIN  | JIS / DIN  |
Diameter Range (mm) | M2-M16 | M3-M16 |
Thread Type | M/MF | M/MF |
Tolerance | 6H | 6H |
Cooling Method | External | External |
Chamfer Type | A | C |
Coating | AlCrN | AlCrN |
Tool Material | HSS-E | HSS-E |
P Steel | ●● | ●● |
M Stainless Steel | ● | ● |
K Cast Iron | ● | ● |
N Non-ferrous Metals | ● | ● |
S Heat-resistant Alloys | | |
H Hardened Materials | | |
Product Parameters: Type C - External Cooling, No Oil Grooves
Model | Thread Spec TD | Pitch P | Chamfer THCHL | Overall Length LF (mm) | Thread Length THLGTH (mm) | Neck Length LU (mm) | Shank Dia DCON (mm) | Square Width K (mm) | Flute Count | Bottom Hole Dia (mm) |
|---|---|---|---|---|---|---|---|---|---|---|
T190 Carbide Forming TapT190-M5-6HXC0-AC | M5 | 0.8 | 2.5P | 70 | 16 | 16 | 6 | 4.9 | / | 4.65 |
T190-M6-6HXC0-AC | M6 | 1 | 80 | 10 | 30 | 6 | 4.9 | / | 5.55 | |
T190-M8X1-6HXC0-AC | M8 | 1 | 90 | 12 | 65 | 6 | 4.9 | / | 7.55 | |
T190-M8-6HXC0-AC | M8 | 1.25 | 90 | 12 | 35 | 8 | 6.2 | / | 7.40 | |
T190-M10X1-6HXC0-AC | M10 | 1 | 90 | 15 | 65 | 7 | 5.5 | / | 9.55 | |
T190-M10-6HXC0-AC | M10 | 1.5 | 100 | 15 | 39 | 10 | 8 | / | 9.30 | |
T190-M12X1.5-6HXC0-AC | M12 | 1.5 | 100 | 15 | 71 | 9 | 7 | / | 11.30 | |
T190-M14X1.5-6HXC0-AC | M14 | 1.5 | 100 | 15 | 71 | 11 | 9 | / | 13.30 | |
T190-M16X1.5-6HXC0-AC | M16 | 1.5 | 100 | 15 | 57 | 12 | 9 | / | 15.30 | |
Cutting Parameters
ISO Group | Material | Brinell Hardness (HB) | Tensile Strength Rm (N/mm²) | Vc Cutting Speed (m/min) T102 | Vc Cutting Speed (m/min) T103 | Vc Cutting Speed (m/min) T109 |
|---|---|---|---|---|---|---|
P | Unalloyed Steel C≤0.25% (Annealed) | 125 | 428 | 15-25 | 8-13 | 35-60 |
0.25<C≤0.55% (Annealed) | 190 | 639 | 10-15 | 7-12 | 30-65 | |
0.25<C≤0.55% Quenched & Tempered | 210 | 708 | 10-15 | 7-12 | 30-65 | |
C>0.55% Annealed | 190 | 639 | 10-15 | 7-12 | 30-65 | |
C>0.55% Quenched & Tempered | 300 | 1013 | 8-13 | 6-9 | 30-65 | |
Free-cutting Steel (Short Chips), Annealed | 220 | 745 | 10-15 | 7-12 | 30-65 | |
Low Alloy Steel, Annealed | 175 | 591 | 10-15 | 7-12 | 35-65 | |
Low Alloy Steel, Quenched & Tempered | 285 | 960 | 3-5 | 3-5 | 25-65 | |
Low Alloy Steel, Quenched & Tempered | 380 | 1282 | | | | |
Low Alloy Steel, Quenched & Tempered | 430 | 1477 | | | | |
High Alloy & High Alloy Tool Steel, Annealed | 200 | 675 | 10-15 | 7-12 | 30-60 | |
High Alloy & High Alloy Tool Steel, Quenched & Tempered | 300 | 1013 | 3-5 | 3-5 | 25-55 | |
High Alloy & High Alloy Tool Steel, Quenched & Tempered | 400 | 1361 | | | | |
M | Stainless Steel Ferritic / Martensitic, Annealed | 200 | 675 | 10-15 | 7-12 | 25-55 |
Stainless Steel Martensitic, Quenched & Tempered | 330 | 1114 | 4-6 | 3-5 | 25-55 | |
Stainless Steel Austenitic, Quenched | 200 | 675 | 8-13 | 5-8 | 25-35 | |
Austenitic Precipitation Hardening Stainless Steel (PH Stainless) | 300 | 1013 | 4-6 | 3-5 | 25-35 | |
Austenitic-Ferritic Duplex Stainless Steel | 230 | 778 | 4-6 | 3-5 | 25-35 | |
K | Malleable Cast Iron Ferritic | 200 | 400 | | | |
Malleable Cast Iron Pearlitic | 260 | 700 | | | | |
Grey Cast Iron Low Tensile Strength | 180 | 200 | | | | |
Grey Cast Iron High Tensile / Austenitic | 245 | 350 | | | | |
Ductile Iron Ferritic | 155 | 400 | 10-20 | 7-12 | 35-55 | |
Ductile Iron Pearlitic | 265 | 700 | 10-20 | 7-12 | 30-50 | |
Compacted Graphite Iron GGV (CGI) | 230 | 400 | | | | |
N | Wrought Aluminum Alloy Non-aged | 30 | - | 15-25 | 10-20 | 60-85 |
Wrought Aluminum Alloy Age-treated | 100 | 340 | 15-20 | 10-15 | 55-70 | |
Cast Aluminum Alloy ≤12%Si, Non-aged | 75 | 260 | 10-20 | 10-15 | 50-75 | |
Cast Aluminum Alloy ≤12%Si, Age-treated | 90 | 310 | 10-20 | 10-15 | 50-65 | |
Cast Aluminum Alloy >12%Si, Non-aged | 130 | 450 | 10-20 | 10-15 | | |
Magnesium Alloy | 70 | 250 | 10-15 | 10-15 | | |
Copper & Copper Alloy (Bronze / Brass) Unalloyed Electrolytic Copper | 100 | 340 | 25-35 | | | |
Brass, Bronze, Red Brass | 90 | 310 | 10-25 | 6-15 | | |
Copper Alloy, Short Chips | 110 | 380 | 15-25 | 10-20 | | |
High Strength Ampco Alloy | 300 | 1010 | | | | |
S | Superalloy Iron-based, Annealed | 200 | 680 | | | |
Superalloy Iron-based, Age-treated | 280 | 940 | | | | |
Superalloy Nickel or Cobalt-based, Annealed | 250 | 840 | | | | |
Superalloy Nickel or Cobalt-based, Age-treated | 350 | 1180 | | | | |
Superalloy Cast | 320 | 1080 | | | | |
Titanium Alloy Pure Ti | 200 | 680 | | | | |
Titanium Alloy α & β Phase, Age-treated | 375 | 1260 | | | | |
Titanium Alloy β Phase | 410 | 1400 | | | | |
Tungsten Alloy | 300 | 1010 | | | | |
Molybdenum Alloy | 300 | 1010 | | | | |
H | Hardened Steel Quenched & Tempered 50HRC | | | | | |
Hardened Steel Quenched & Tempered 55HRC | | | | | | |
Hardened Steel Quenched & Tempered 60HRC | | | | | | |
Hardened Cast Iron Quenched & Tempered 55HRC | | | | | |