End Mills
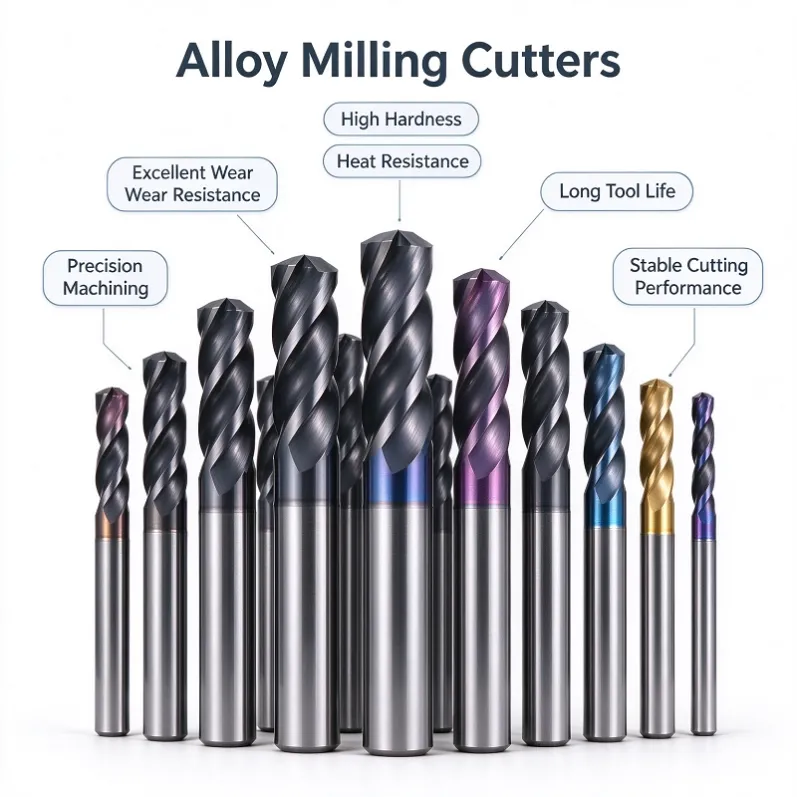
Solid Carbide End Mills
End mills are multi-edge rotary cutting tools for workpiece machining. During operation, the tool performs the primary rotary motion, while the workpiece feeds; alternatively, the workpiece can be fixed and the tool moved to complete cutting.
Specifications
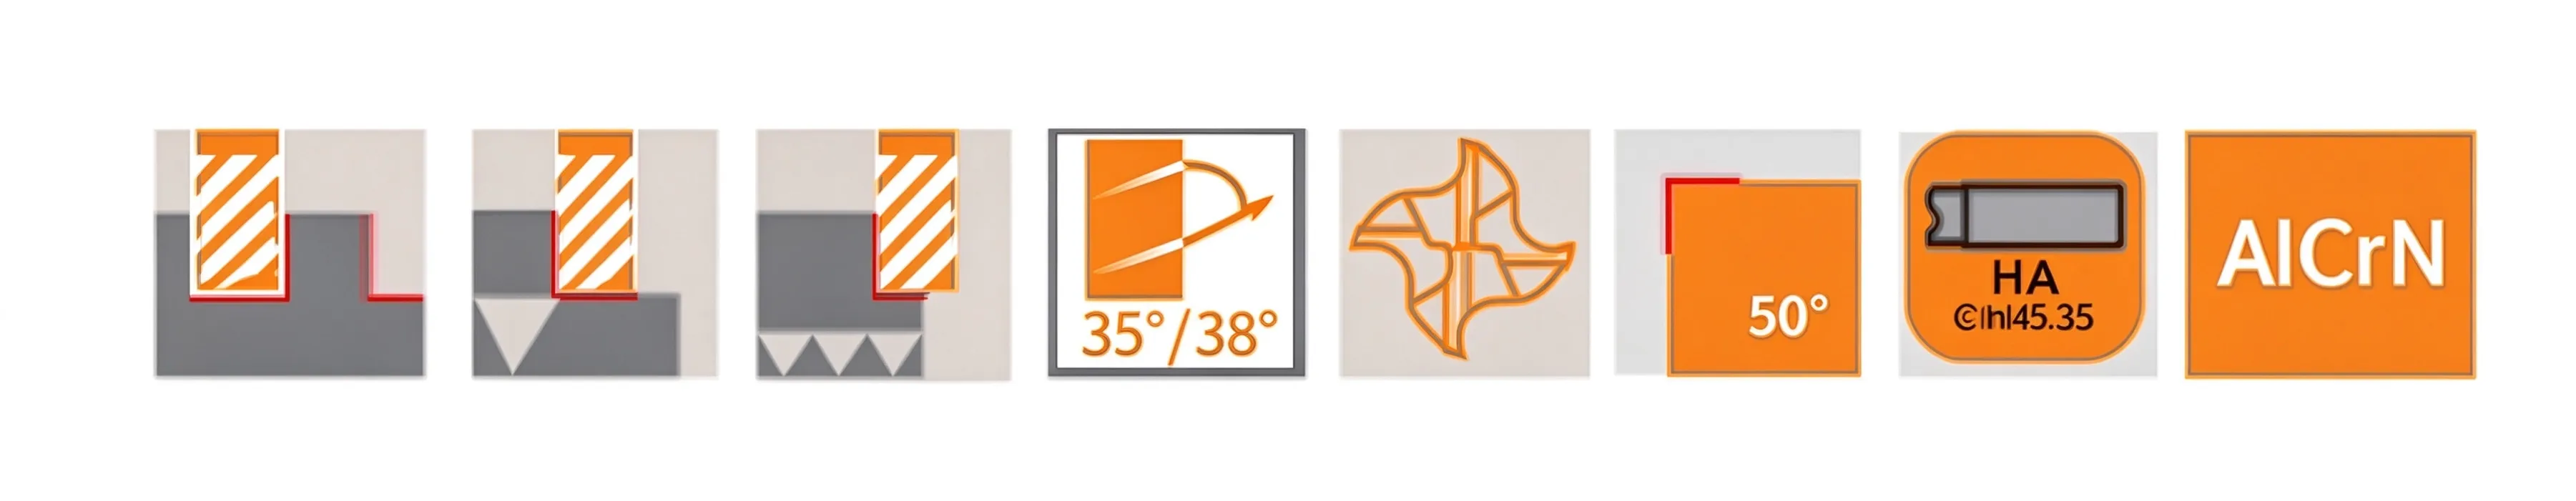
- Climb Milling:
- Chip thickness reduces from thick to thin, lowering tool wear.
- Conventional Milling:
- Chip thickness grows from zero to thick, which may induce work hardening and vibration.
- ISO workpiece material groups:
- P, M, K, S
Machining Methods
Side milling, slotting, helical interpolation milling, ramping, dynamic milling, peripheral milling, full slotting, cavity milling, helical plunge milling, form milling
Applications
Aerospace & Energy industries
Key Features
- Styles: Flat bottom, ball nose, corner radius, corner chamfer, close pitch teeth
- 2, 3, 4 or 6 cutting flutes
- Diameter range: 1–20 mm & 0.125–1 inch
- New substrate material with AlCrN coating, greatly improves wear resistance and extends tool service life
Tool Grade Classification Table
Picture | Grade | Flutes (Z) | Helix Angle | Cutting method | Cutting Edge Tolerance | Diameter (mm) | Diameter (inch) | Material & Application | Max Hardness |
|---|---|---|---|---|---|---|---|---|---|
 | ECO | 2 | 35° |  | h9 | 1–20 | - | General purpose. For carbon steel, tool steel, alloy steel | HRC45 |
 | ECO | 4 | 35°/38° |  | h9 | 1–20 | 0.125–1 | General purpose. 4 flutes deliver superior surface finish. Unequal helix & unequal pitch design for excellent vibration resistance. | HRC45 |
 | ECO | 4 | 35°/38° |  | h9 | 4–20 | - | General purpose. Corner chamfer prevents chipping in high-speed cutting. Unequal helix & unequal pitch for vibration damping. | HRC45 |
 | ECO | 4 | 35°/38° |  | h9 | 1–20 | 0.125–1 | General purpose. Corner radius protects against high-speed chipping. Unequal helix & unequal pitch for vibration resistance. 4-flute design. | HRC45 |
 | ECO | 2 | 30° |  | h7 | 1–20 | 0.125–1 | General purpose. For round-bottom grooving & special profiling. Better chipping resistance. | HRC45 |
 | ECO | 6 | 45° |  | h9 | 6–20 | - | General purpose. Close pitch teeth for high-speed & high-feed finish milling, ideal for side finishing. | HRC45 |
 | ECO | 2 | 45° |  | h8 | 3–20 | 0.125–1 | Aluminum alloy. Vibration-resistant design, special edge treatment for high surface quality. | - |
 | ECO | 3 | 37°/39°/41° |  | h8 | 3–20 | - | Aluminum alloy. Unequal helix & unequal pitch, anti-vibration, special edge treatment for superior surface finish. | - |
| ECO | 3 | 45° |  | h8 | 4–20 | - | Aluminum alloy. Unequal pitch, vibration-resistant, special edge treatment for high surface quality. | - |
Tool parameters
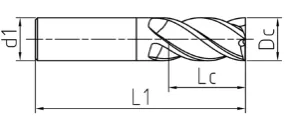
Tool Dimensions & Ordering List
Order No. | Dc(mm) | d1(mm) | Lc(mm) | L1(mm) | Z (Flutes) | Work Material | Hardness |
|---|---|---|---|---|---|---|---|
M200-4ES-010 | 1 | 4 | 3 | 50 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-015 | 1.5 | 4 | 4 | 50 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-020 | 2 | 4 | 6 | 50 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-025 | 2.5 | 4 | 8 | 50 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-030 | 3 | 4 | 8 | 50 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-030P | 3 | 6 | 8 | 50 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-035 | 3.5 | 4 | 11 | 50 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-040 | 4 | 4 | 12 | 50 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-040P | 4 | 6 | 12 | 50 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-045 | 4.5 | 6 | 12 | 50 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-050 | 5 | 6 | 13 | 50 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-055 | 5.5 | 6 | 16 | 50 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-060 | 6 | 6 | 16 | 50 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-065 | 6.5 | 8 | 16 | 60 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-070 | 7 | 8 | 20 | 60 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-075 | 7.5 | 8 | 20 | 60 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-080 | 8 | 8 | 20 | 60 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-085 | 8.5 | 10 | 23 | 75 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-090 | 9 | 10 | 23 | 75 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-095 | 9.5 | 10 | 25 | 75 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-100 | 10 | 10 | 25 | 75 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-110 | 11 | 12 | 28 | 75 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-120 | 12 | 12 | 30 | 75 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-140 | 14 | 14 | 34 | 100 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-160 | 16 | 16 | 36 | 100 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-180 | 18 | 18 | 40 | 100 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
M200-4ES-200 | 20 | 20 | 45 | 100 | 4 | Carbon steel, alloy steel, ductile iron, grey cast iron | HRC45 |
Machining Parameter Table
ISO Material Group | Condition | HB / HRC | Tensile Strength(N/mm²) | Cutting Speed Vc(m/min) | fz mm/tooth | 2mm | 4mm | 6mm | 8mm | 10mm | 12mm | 14mm | 16mm |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
Unalloyed Steel C≤0.25% | Annealed | 125 | 428 | 45~80 | 0.01 | 0.02 | 0.04 | 0.06 | 0.060 | 0.06 | 0.07 | 0.07 | 0.07 |
Unalloyed Steel 0.25<C≤0.55% | Annealed | 190 | 639 | 45~75 | 0.01 | 0.02 | 0.04 | 0.06 | 0.060 | 0.06 | 0.07 | 0.07 | 0.07 |
Unalloyed Steel 0.25<C≤0.55% | Quenched & Tempered | 210 | 708 | 45~75 | 0.01 | 0.02 | 0.04 | 0.06 | 0.060 | 0.06 | 0.07 | 0.07 | 0.07 |
Unalloyed Steel C>0.55% | Annealed | 190 | 639 | 45~75 | 0.01 | 0.02 | 0.04 | 0.06 | 0.060 | 0.06 | 0.07 | 0.07 | 0.07 |
Unalloyed Steel C>0.55% | Quenched & Tempered | 300 | 1013 | 40~60 | 0.01 | 0.02 | 0.03 | 0.05 | 0.052 | 0.05 | 0.06 | 0.06 | 0.06 |
Free-cutting Steel (short chip) | Annealed | 220 | 745 | 45~65 | 0.01 | 0.02 | 0.04 | 0.06 | 0.060 | 0.06 | 0.07 | 0.07 | 0.07 |
Low Alloy Steel | Annealed | 175 | 591 | 45~75 | 0.01 | 0.02 | 0.04 | 0.06 | 0.060 | 0.06 | 0.07 | 0.07 | 0.07 |
Low Alloy Steel | Quenched & Tempered | 300 | 1013 | 40~60 | 0.01 | 0.02 | 0.03 | 0.05 | 0.052 | 0.05 | 0.06 | 0.06 | 0.06 |
Low Alloy Steel | Quenched & Tempered | 380 | 1282 | 40~60 | 0.01 | 0.02 | 0.03 | 0.05 | 0.052 | 0.05 | 0.06 | 0.06 | 0.06 |
Low Alloy Steel | Quenched & Tempered | 430 | 1477 | 30~40 | 0.01 | 0.02 | 0.03 | 0.04 | 0.045 | 0.05 | 0.05 | 0.05 | 0.06 |
High Alloy / Tool Steel | Annealed | 200 | 675 | 45~75 | 0.01 | 0.02 | 0.04 | 0.06 | 0.060 | 0.06 | 0.06 | 0.06 | 0.06 |
High Alloy / Tool Steel | Quenched & Tempered | 300 | 1013 | 40~60 | 0.01 | 0.02 | 0.04 | 0.05 | 0.052 | 0.05 | 0.06 | 0.06 | 0.06 |
High Alloy / Tool Steel | Quenched & Tempered | 400 | 1361 | 40~60 | 0.01 | 0.02 | 0.03 | 0.04 | 0.042 | 0.04 | 0.05 | 0.05 | 0.05 |
Stainless Steel Ferritic / Martensitic | Annealed | 200 | 675 | 35~40 | 0.01 | 0.02 | 0.04 | 0.06 | 0.060 | 0.06 | 0.06 | 0.06 | 0.06 |
Stainless Steel Martensitic | Quenched & Tempered | 330 | 1114 | 30~35 | 0.01 | 0.02 | 0.04 | 0.05 | 0.052 | 0.05 | 0.06 | 0.06 | 0.06 |
Stainless Steel Austenitic | Quenched | 200 | 675 | 30~35 | 0.01 | 0.02 | 0.04 | 0.04 | 0.050 | 0.05 | 0.06 | 0.06 | 0.06 |
Precipitation Hardening Stainless (PH) | - | 300 | 1013 | 30 | 0.01 | 0.02 | 0.03 | 0.03 | 0.035 | 0.04 | 0.04 | 0.05 | 0.05 |
Duplex Stainless Steel (Austenitic-Ferritic) | - | 230 | 778 | 30~35 | 0.01 | 0.02 | 0.04 | 0.04 | 0.050 | 0.05 | 0.06 | 0.06 | 0.06 |
Malleable Cast Iron Ferritic | - | 200 | 400 | 55~60 | 0.01 | 0.02 | 0.04 | 0.06 | 0.071 | 0.07 | 0.08 | 0.08 | 0.09 |
Malleable Cast Iron Pearlitic | - | 260 | 700 | 55~60 | 0.01 | 0.02 | 0.04 | 0.06 | 0.071 | 0.07 | 0.08 | 0.08 | 0.09 |
Grey Cast Iron Low Tensile | - | 180 | 200 | 55~60 | 0.01 | 0.02 | 0.04 | 0.06 | 0.071 | 0.07 | 0.08 | 0.08 | 0.09 |
Grey Cast Iron High Tensile/Austenitic | - | 245 | 350 | 55~60 | 0.01 | 0.02 | 0.04 | 0.06 | 0.071 | 0.07 | 0.08 | 0.08 | 0.09 |
Ductile Iron Ferritic | - | 155 | 400 | 55~60 | 0.01 | 0.02 | 0.04 | 0.05 | 0.060 | 0.06 | 0.07 | 0.08 | 0.08 |
Ductile Iron Pearlitic | - | 265 | 700 | 45~55 | 0.01 | 0.01 | 0.04 | 0.05 | 0.055 | 0.06 | 0.07 | 0.07 | 0.07 |
Compacted Graphite Iron (CGI) | - | 230 | 400 | 55~60 | 0.01 | 0.02 | 0.04 | 0.05 | 0.060 | 0.06 | 0.07 | 0.08 | 0.08 |
Wrought Aluminum Alloy Non-aged | - | 30 | - | - | - | - | - | - | - | - | - | - | - |
Wrought Aluminum Alloy Aged | - | 100 | 340 | - | - | - | - | - | - | - | - | - | - |
Cast Al Alloy ≤12%Si Non-aged | - | 75 | 260 | - | - | - | - | - | - | - | - | - | - |
Cast Al Alloy ≤12%Si Aged | - | 90 | 310 | - | - | - | - | - | - | - | - | - | - |
Cast Al Alloy >12%Si Non-aged | - | 130 | 450 | - | - | - | - | - | - | - | - | - | - |
Magnesium Alloy | - | 70 | 250 | - | - | - | - | - | - | - | - | - | - |
Copper & Copper Alloys | - | 100~300 | 310~1010 | - | - | - | - | - | - | - | - | - | - |
Heat-resistant Alloys Iron-base | Annealed | 200 | 680 | - | - | - | - | - | - | - | - | - | - |
Heat-resistant Alloys Iron-base | Aged | 280 | 940 | - | - | - | - | - | - | - | - | - | - |
Heat-resistant Alloys Ni/Co-base | Annealed | 250 | 840 | - | - | - | - | - | - | - | - | - | - |
Heat-resistant Alloys Ni/Co-base | Aged | 350 | 1180 | - | - | - | - | - | - | - | - | - | - |
Heat-resistant Alloys Ni/Co-base | Cast | 320 | 1080 | - | - | - | - | - | - | - | - | - | - |
Titanium Alloy Pure Ti | - | 200 | 680 | - | - | - | - | - | - | - | - | - | - |
Titanium Alloy α+β Aged | - | 375 | 1260 | - | - | - | - | - | - | - | - | - | - |
Titanium Alloy β | - | 410 | 1400 | - | - | - | - | - | - | - | - | - | - |
Tungsten Alloy | - | 300 | 1010 | - | - | - | - | - | - | - | - | - | - |
Molybdenum Alloy | - | 300 | 1010 | - | - | - | - | - | - | - | - | - | - |
Hardened Steel | Quenched & Tempered | 50HRC | - | - | - | - | - | - | - | - | - | - | - |
Hardened Steel | Quenched & Tempered | 55HRC | - | - | - | - | - | - | - | - | - | - | - |
Hardened Steel | Quenched & Tempered | 60HRC | - | - | - | - | - | - | - | - | - | - | - |
Hardened Cast Iron | Quenched & Tempered | 50HRC | - | - | - | - | - | - | - | - | - | - | - |